More than 50 years of combined experience in high-purity chemistry, process development and commercial manufacturing.
Specialty chemistry
Organic peroxides, masterbatches, precious-metal complexes, ligands and specialty chemicals.
Development to manufacture
Custom design, synthesis and scale-up, supported by practical project expertise.
Scientific expertise
A multidisciplinary team in catalysis, process chemistry and advanced materials.
Industrial applications
Supporting pharmaceuticals, polymers, agrochemicals, aroma chemicals, semiconductors and petrochemicals.
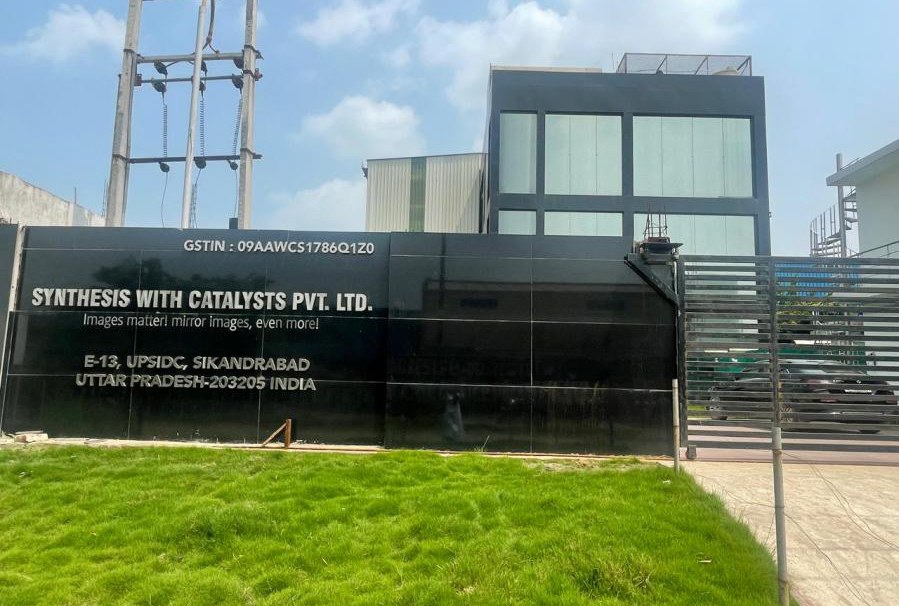
Our manufacturing site · Sikandrabad, Uttar Pradesh
Engineered in India
From Indian manufacturing to global supply.
Founded
2015
Years of combined experience
50+
ISO certifications
3
Catalog products
137
Our purpose
Scientificexcellence.Responsibleprogress.
Our vision
To become a globally respected leader in advanced catalyst technologies, recognised for scientific excellence, uncompromising quality and trusted partnerships.
Innovating Chemistry.Advancing Industry.Creating a Sustainable Future.
Advance chemistry
Develop high-purity catalysts and specialty chemicals that improve efficiency and selectivity.
Scientific excellence
High purity
Performance
Manufacture responsibly
Use resources efficiently, reduce waste and build responsible manufacturing into process development.
Cleaner chemistry
Resource efficiency
Build Indian technology
Create competitive chemical technologies that strengthen Indian manufacturing and serve global industry.
Make in India
Indigenous innovation
Our evolution
Fromresearchtocommercialscale.
2015
Foundation & vision
SWC began with a clear focus on scientific excellence in catalyst chemistry.
2018–19
R&D & scale-up
In-house research, analytics and application testing supported scalable manufacturing.
2020–21
Innovation to market
Commercialisation accelerated alongside stronger industry and international engagement.
Today
Expanded expertise
The portfolio now spans precious-metal catalysts, chiral chemistry and high-performance organic peroxides.
Leadership
Scientificexperienceconnectedtoindustryexecution.
A multidisciplinary leadership team combining catalyst chemistry, process development, commercial manufacturing and operations.
AP
Aksshay R. Parmaar
Founder & CMD
RP
Ms. Rakhi Parmar
Director
DS
Leadership team
Divyanshi Saran
Director
DR
Leadership team
Devender S Rauthan
VP – Operations
Our capabilities
Onepathfromdevelopmenttomanufacture.
R&D & Process Development
Custom synthesis & route development
Catalyst & ligand development
Process optimisation
Application-focused development
Analytical & Quality
In-house QC & analytical testing
GC, HPLC & polarimetry
Moisture & purity analysis
External laboratory support
Pilot & Scale-up
Gram-to-kilogram scale-up
Process optimisation
Pilot-scale validation
Technology transfer
Manufacturing
GLR & SS316 reactor systems
Autoclave capabilities
Vacuum distillation & centrifugation
Chilling & automated safety systems
R&D infrastructure
Practical process development, from bench to transfer.
Reaction workstationsStirrers, heating mantles, laboratory distillation and vacuum filtration
Fume-hood infrastructureSix hoods, including two walk-in units with utility gases and plumbing
Separation systemsLaboratory centrifuge, sonicator and vacuum oven
Solvent recovery23 L, 5 L and 2 L rotavapor capability
Thermal processingMuffle furnace rated to 1200 °C and drying oven
Automated safetyFire and gas-leak alarms with sprinkler protection
Manufacturing infrastructure
Flexible equipment from glass reactors to commercial systems.
Glass-lined reactorsTwo 1.2 kL and five 2 kL systems with heating, chilling and distillation
SS316 reactorsThree 3 kL systems with heating, chilling and high-vacuum distillation
Glass reactorsTwelve 100 L systems for development and flexible production
Separation and recoveryHigh-vacuum distillation, SS centrifuges and 1500 L / 500 L rotary evaporators
Temperature control20 TR chilling systems, brine tank and cold-room capability to −30 °C
Utilities and environmental supportRO, DM-water and 500 L/hr ETP systems
 Our vision
 R&D infrastructure
 Manufacturing infrastructure